
Can Packaging
Can Filler Seamer Integration Guide
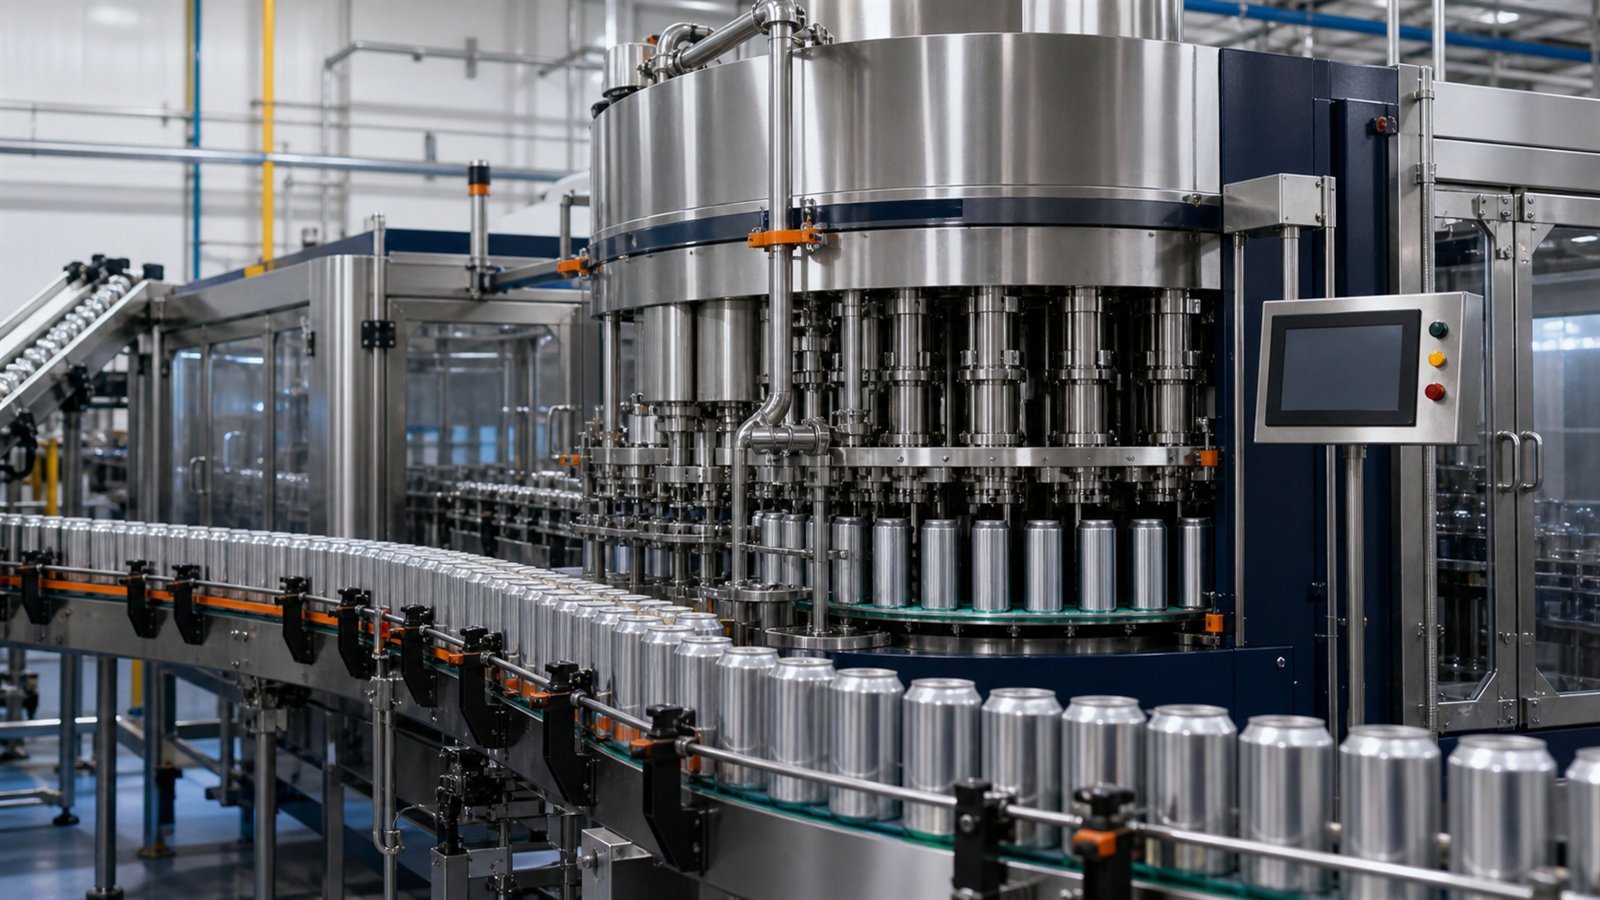
A filler-seamer block must synchronize can pitch, product filling, lid placement, lift pressure, chuck and roll setup and discharge. The shortest possible open-can transfer helps protect product but demands precise controls.
Practical buyer guide | Updated October 3, 2026 | Final scope must be verified through drawings, samples and agreed acceptance tests
Editorial basis
Planning guidance, not a final machine specification
Published by Allot Tech (Suzhou) Co., Ltd. This multilingual library uses a consistent buyer-decision framework and independently prepared language packs. Confirm the final configuration against supplier drawings, actual product and packaging samples, destination requirements and the signed technical agreement.
Direct answer
What this decision means for a real filling project
A filler-seamer block must synchronize can pitch, product filling, lid placement, lift pressure, chuck and roll setup and discharge. The shortest possible open-can transfer helps protect product but demands precise controls.
This guide is part of the Can Filling Line Buyer Guide cluster. Read the hub when the project still needs a broader comparison.
Filler-seamer integration: an interface and test plan
A filler and seamer can each meet an individual speed claim while the connected cell loses product or creates excessive rejects. Write the handover conditions between them into the purchase specification. The document should name the responsible supplier, the test method and the record needed to close each interface.
| Interface | Freeze before manufacture | Record during the trial |
|---|---|---|
| Filler discharge to seamer infeed | Can drawing, pitch, transfer parts, speed coordination and permitted handling conditions. | Can stability, spills, flange condition and transfer behaviour at the agreed rates. |
| End supply and lid placement | Approved end, feed arrangement, low-level response and missing-end handling. | End-feed reliability, replenishment response and the safe controlled response to an agreed fault simulation. |
| Stops and restart | Stop signals, open-can disposition, restart sequence and responsibilities for retained product. | Stop cause, time, affected quantity and checks required before good product is counted again. |
| Inspection and rejects | Inspection scope, count point, reject confirmation and separation of held or rejected cans. | Challenge result, rejected quantity and agreement between the counter and physical output. |
| Format change and cleaning | Parts list, recipes, cleaning boundary, tools, trained personnel and release checks. | Elapsed change time, restored settings and fill, seam and handling results after restart. |
Which configurations should the acceptance trial cover?
Create one row for each approved product, can and end combination. Mark the planned tests for startup, steady running, a controlled downstream stop, end replenishment and restart. Add a format change if multiple formats are included in the order. Use real operating conditions or document how a test substitute limits the conclusion.
Each test row needs a target condition, an instrument or observation method, a duration or sample plan, an acceptance criterion, a result and an owner. Safety-related tests must follow the equipment supplier’s approved procedure and be conducted by qualified personnel. Do not bypass guards or introduce improvised obstructions to create a fault.
Worked example: accepted output versus a speed setting
Illustration only: during a defined 20-minute test, 1,600 cans reach the agreed inspection count point. Forty are rejected and the remaining 1,560 meet the agreed criteria. Accepted output for that test is 1,560 / 20 x 60 = 4,680 good cans per hour. Report the 40 rejects and any stops alongside that result.
Extrapolating a short test does not prove shift-long performance. Agree a representative duration and the treatment of planned stops before testing. Do not subtract reject quantities twice or count held product as accepted. Compare FAT results with the installed line’s SAT because site utilities and downstream equipment may differ.
What if the filler and seamer come from different suppliers?
Name one integration lead in the purchase documents. Ask both parties to approve transfer drawings, signals, operating sequence, cleaning boundaries and the format list. Record who will diagnose an interface fault and who supplies each change part. A generic statement that the machines are compatible is not a substitute for an agreed connected-cell test.
What evidence should accompany handover?
- The approved product, can, end and format matrix, with drawing and specification revisions.
- As-built transfer and utility drawings, the interface signal list and the agreed stop/restart procedure.
- Test records identifying samples, settings, duration, good output, rejects and open actions.
- Seam records linked to the trial, manuals, identified change parts and the training handover.
Continue with the can filling machine selection page or the double seam inspection checklist. For another format, use the can format changeover guide.
Technical reference: the Krones filler-seamer block overview illustrates an integrated architecture. Its model-specific features and output figures are not specifications for Allot Tech equipment.
Engineering inputs
Define the duty before comparing equipment
A useful proposal starts from agreed process and package information. These inputs keep suppliers from filling gaps with incompatible assumptions.
Send these details
- Product temperature and gas
- Can and end specifications
- Fill and headspace
- Seamer tooling
- Target speed
Require these checks
- Measure fill and foam
- Verify lid feed
- Complete first- and second-operation seam checks
- Test stops without open-can backlog
Line integration
Connect the choice to upstream and downstream equipment
Project decision record
Turn the topic into four controlled project decisions
A useful guide should change the RFQ, proposal and acceptance plan. Use this record to keep the buyer, equipment supplier and site team on the same basis.
Freeze the application basis
Freeze the product conditions, can and end drawings, fill quantity and approved format list. Identify the party responsible for each interface.
Define rated and sustained duty
Agree the count point, test duration and treatment of stops, rejects and held cans. Keep machine speed separate from accepted connected-cell output.
Control line interfaces
Approve the transfer parts, signals, end-feed response, cleaning boundary and restart procedure before the equipment is released for manufacture.
Approve measurable evidence
Retain fill and seam results from the same trial, plus the stop log and open-item record. Identify who closes each issue before shipment.
Comparison sheet
Put every supplier on the same basis
| Decision area | What to state in the RFQ | What to verify |
|---|---|---|
| Product conditions | product temperature and gas | measure fill and foam |
| Can and end | can and end specifications | verify lid feed |
| Fill and closure | fill and headspace | complete first- and second-operation seam checks |
| Stops and restart | seamer tooling | test stops without open-can backlog |
| Project scope | Utilities, interfaces, documents, spares, packing, shipping and support | Written inclusions, exclusions and acceptance evidence |
Verification route
Move from a claim to recorded evidence
- Approve the duty, drawings and test conditions before fabrication is treated as final.
- Use production-intent product and packaging wherever they materially affect performance.
- Record results by format, operating condition and quality criterion rather than relying on a short edited video.
- List open items, owners and closure evidence before packing and again after site commissioning.
Risk register
Resolve these risks before price becomes the deciding factor
Low quotations often hide different assumptions. A short written risk register makes technical and commercial differences visible before contract award.
| Risk | Why it matters here | Required control |
|---|---|---|
| Application mismatch | Filling conditions and closing quality must be verified together. | Approve the product, can and end basis and record fill, foam and seam results during the connected trial. |
| Package or format mismatch | Different cans or ends can change transfer and seaming requirements. | Approve the format matrix and demonstrate the specified handling parts, lid feed and tooling. |
| Line imbalance | An end-feed or downstream stop can interrupt the complete filling cell. | Test the agreed controlled stop, open-can disposition and restart sequence. |
| Weak acceptance evidence | A speed display does not establish accepted product output. | Record test duration, count point, rejects, held cans and owner-approved close-out evidence. |
Buyer questions
Answers to common RFQ and acceptance questions
When is Can Filler Seamer Integration Guide useful?
Can lines where filling and seaming are purchased as one integrated machine or closely coupled cell. Good filler results cannot compensate for incorrect lids, poor seam setup or contaminated flanges.
What details should be supplied before requesting a quotation?
Prepare the following project-specific information: product temperature and gas, can and end specifications, fill and headspace, seamer tooling, target speed. Drawings, photos and representative samples help the engineering review move from a budget assumption to a defined scope.
How should the proposed solution be checked before acceptance?
Use an agreed review or test plan to measure fill and foam, verify lid feed, complete first- and second-operation seam checks, test stops without open-can backlog. Record the conditions, measurements and open actions so the result can be compared with the approved specification.
What should the supplier proposal state for can filler seamer machine?
The proposal should state the design basis, included equipment, utilities, interfaces, output conditions, change parts, documentation, spare parts, delivery boundary and acceptance method. For this topic, explicitly record product temperature and gas and can and end specifications.
What evidence should be retained after FAT and site handover?
Retain the approved specification, drawings, test conditions, measured results, alarm and safety checks, open-item register, manuals, backups, parts list and signed handover record. This guide particularly requires evidence for measure fill and foam and verify lid feed.
One-Stop Beverage Equipment Solutions
Send the liquid, bottle, output and destination
Allot Tech (Suzhou) Co., Ltd. was founded in 2019. Our roots are in new-media and online communication; since 2025, we have combined that experience with China manufacturing sourcing to introduce practical beverage and liquid-packaging equipment to global buyers honestly and clearly.